
In many chemical and pharmaceutical processes, solvents are an essential part of production—but they can also become a significant operating cost when they leave the process with wastewater, mother liquor or spent streams.
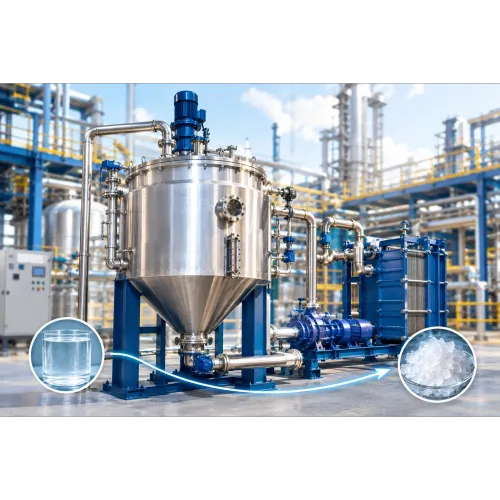
A well-designed solvent recovery system can separate and recover these solvents for reuse, reducing solvent purchase, waste generation and overall operating costs.
At Centpro Engineering, solvent recovery systems are engineered around the actual process stream, solvent properties, required recovery, product purity and available utilities. The objective is not simply to install a distillation column, but to develop a complete separation system that works efficiently under real plant conditions.
Understanding the Solvent Recovery Process
The first step is understanding what needs to be separated.
Solvent-containing streams can vary significantly in composition, concentration and temperature. The relative volatility of the solvent and other components determines the difficulty of separation and influences the required distillation column, number of stages, reflux ratio and operating pressure.
For heat-sensitive or high-boiling solvents, vacuum distillation can be considered to reduce the boiling temperature and protect the product from excessive thermal exposure.
Distillation for Solvent Separation
Distillation is one of the most widely used technologies for industrial solvent recovery.
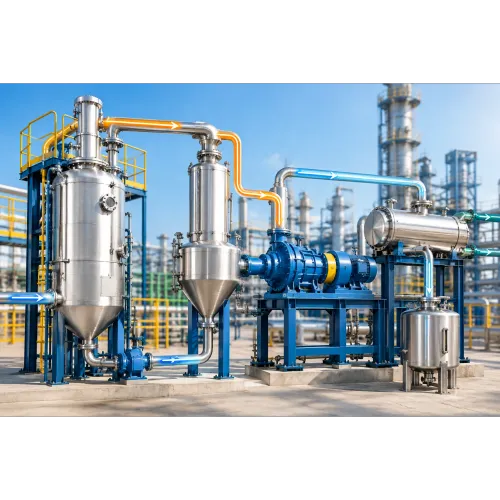
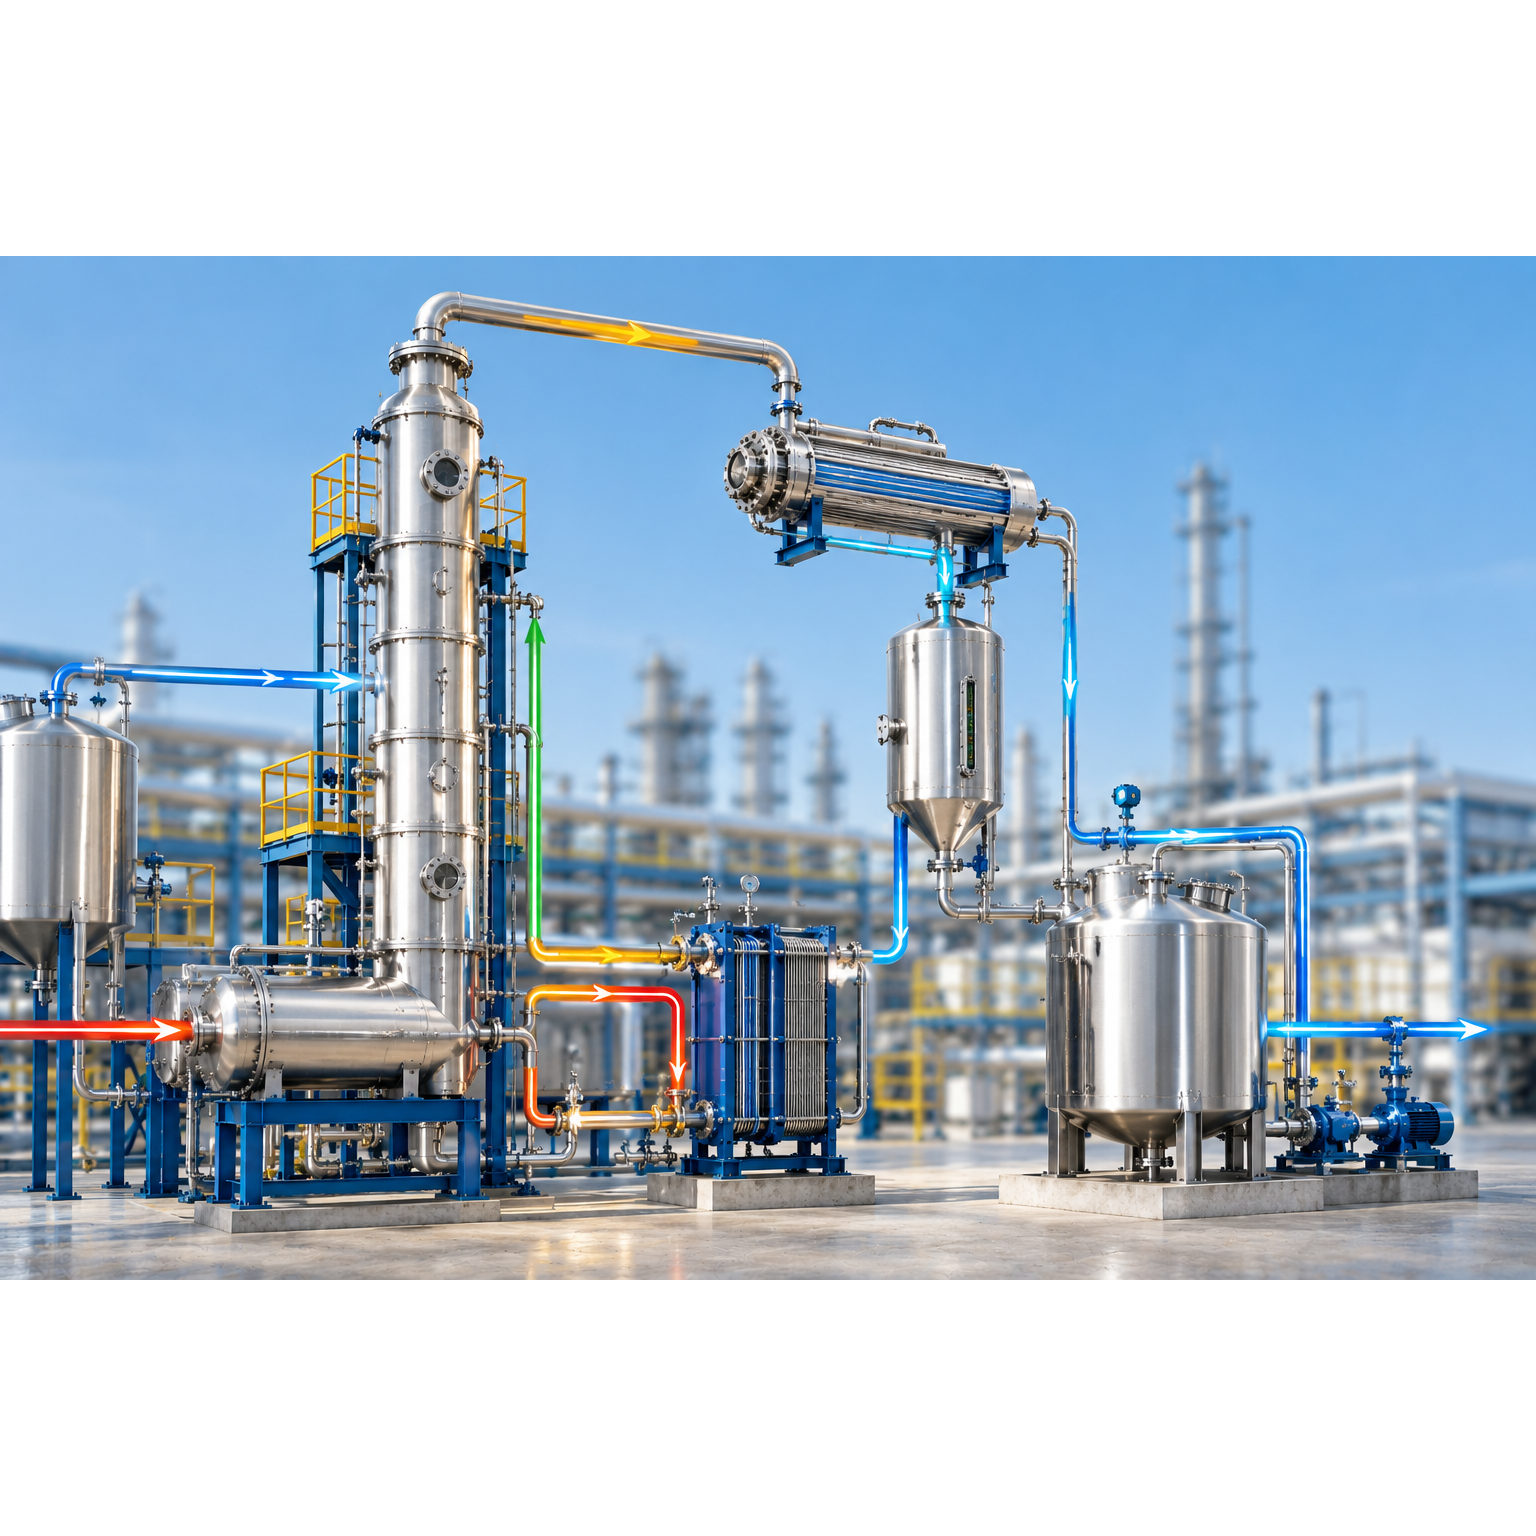
The feed is heated in a reboiler, generating vapour that travels through the column. Depending on the volatility difference, the more volatile solvent can be concentrated toward the top of the column while heavier components remain toward the bottom.
Column configuration, tray or packing selection, reflux ratio, feed condition and operating pressure all influence the final solvent recovery and purity.
For multi-component streams, the separation becomes more complex and may require additional stages or carefully designed fractionation systems.
Condensation and Solvent Recovery
The vapour leaving the distillation column must be efficiently condensed to recover the separated solvent.
The condenser therefore plays a critical role in the overall system. Cooling-medium temperature, solvent properties, vapour load, non-condensable gases and required recovery temperature influence condenser design.
Proper condensation can also reduce solvent losses through the vent system and improve overall recovery.
Heat Integration Can Improve Economics
Energy consumption is an important consideration in solvent recovery.
Reboilers require thermal energy, while condensers reject heat to cooling water or another utility. Heat integration can help recover part of this energy and use it elsewhere in the process.
For example, hot recovered streams may be used to preheat incoming feed, reducing the duty required in the reboiler. The optimum configuration depends on the process temperatures and available heat sources and sinks.
The objective is to balance solvent recovery, product purity, steam consumption, cooling requirements and overall operating cost.
Designing for the Actual Process
Solvent recovery is not a one-size-fits-all application. Solvent composition, boiling point, relative volatility, concentration, viscosity, feed flow rate, operating pressure and required recovery percentage must all be evaluated during process design.
Material compatibility is equally important, particularly when recovering aggressive solvents or handling pharmaceutical and specialty chemical streams.
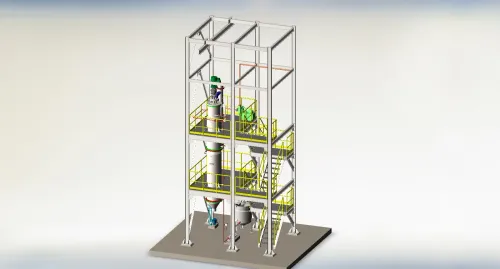
CentPro Engineering supports solvent recovery projects through process design, distillation system engineering, equipment manufacturing, heat integration, instrumentation, installation and commissioning.
Recover More. Waste Less.
A properly engineered solvent recovery system can turn a waste stream into a recoverable process resource.
Share your solvent type, feed composition, flow rate, solvent concentration, required purity and recovery target with Centpro Engineering. Our process engineering team can evaluate the separation requirement and develop a suitable solvent recovery system for your application.
Enquire with Centpro Engineering for customised solvent recovery, distillation and chemical separation solutions.