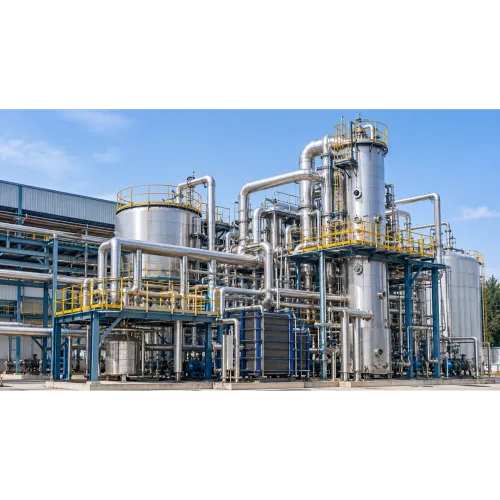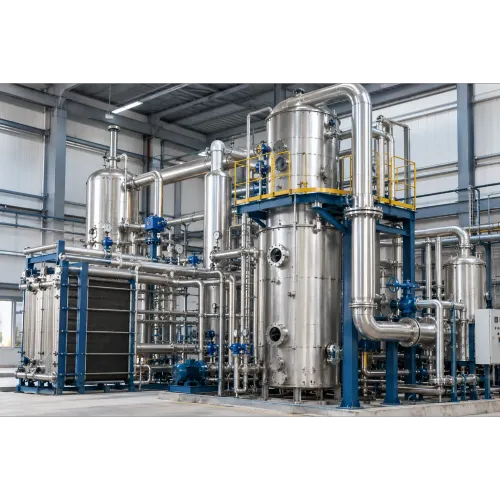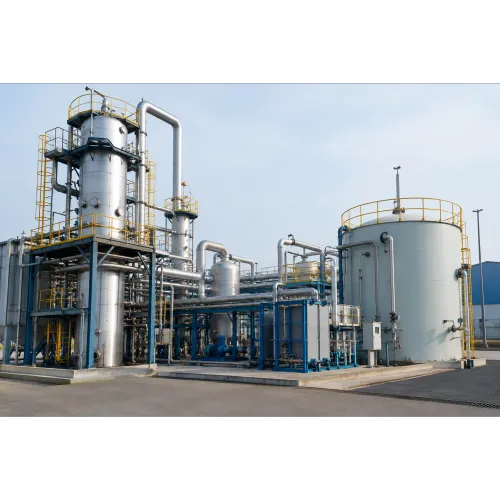

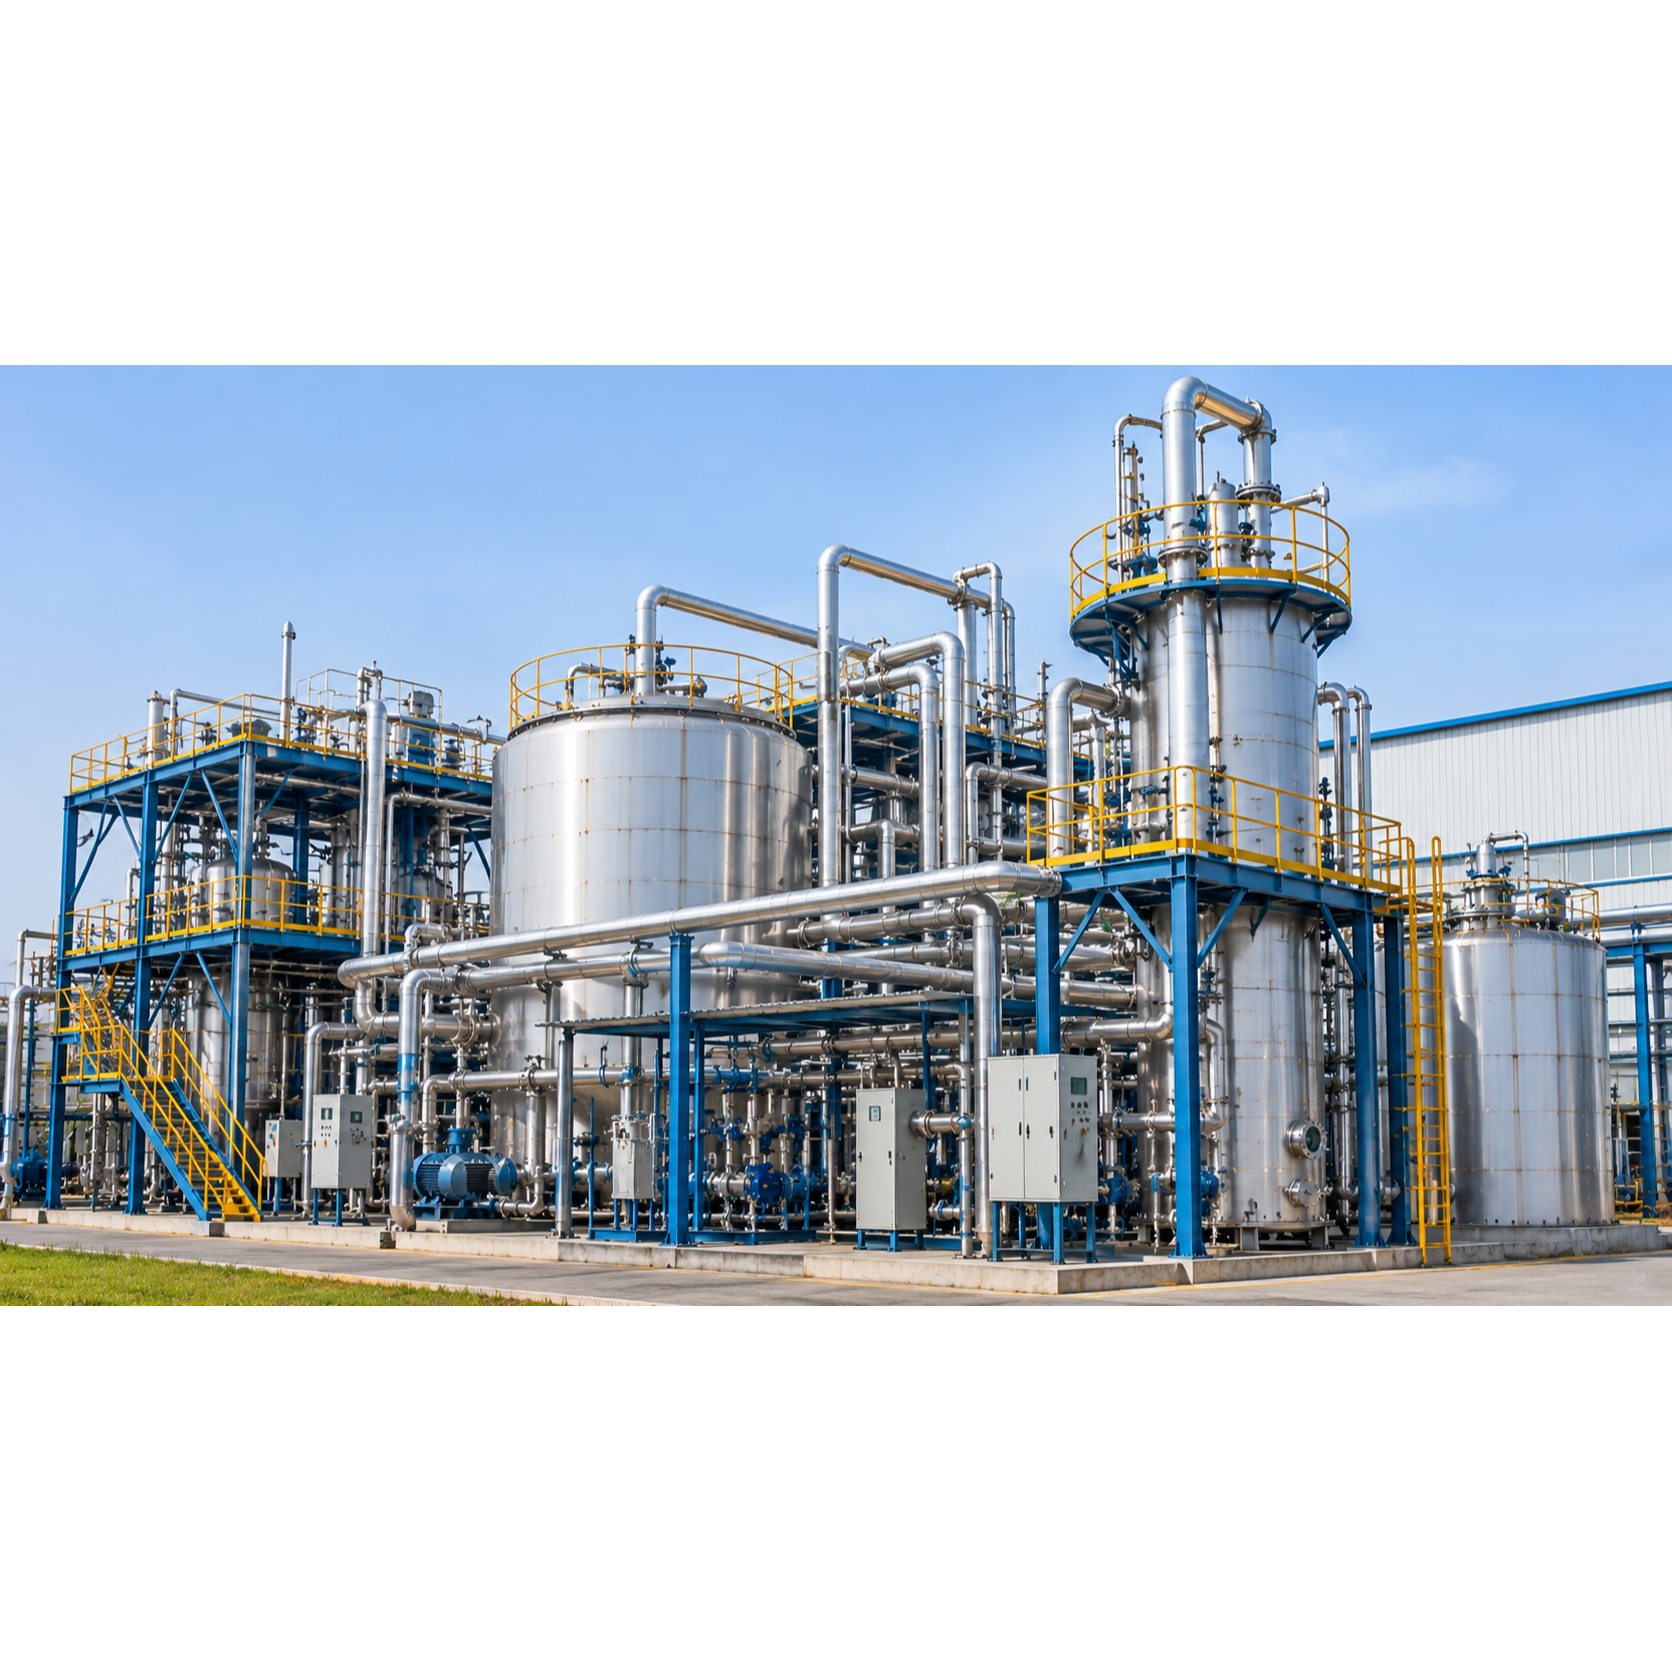
Industrial wastewater containing high Chemical Oxygen Demand (COD) and Total Dissolved Solids (TDS) presents complex challenges for conventional treatment and thermal evaporation systems. Such effluents are commonly encountered in chemical manufacturing, pharmaceutical production, textile processing, specialty chemicals and other industries handling concentrated process streams.
High organic loading combined with elevated dissolved salts can influence wastewater viscosity, foaming tendency, scaling potential and heat-transfer performance. These characteristics directly affect equipment selection, pretreatment requirements and the overall efficiency of an industrial wastewater treatment system.
Treating high-COD, high-TDS effluent requires an integrated process approach because organic compounds and dissolved solids interact differently during concentration, evaporation and downstream separation.
1. COD Characteristics: Understand the Organic Load
Chemical Oxygen Demand (COD) indicates the amount of oxygen equivalent required to chemically oxidise organic and certain inorganic substances present in wastewater.
High-COD effluent may contain solvents, oils, organic acids, process residues, surfactants and other dissolved or suspended compounds. Their behaviour during treatment depends on biodegradability, volatility, thermal stability and chemical composition.
Important design considerations include:
Total and soluble COD concentration
Biodegradable and non-biodegradable organic fractions
Presence of volatile organic compounds (VOCs)
Oil, grease and suspended organic matter
Thermal stability and potential decomposition
Compatibility with biological, chemical and membrane treatment
Biological treatment may be suitable for biodegradable organic loads, while physicochemical treatment or other specialised processes may be required for difficult or inhibitory compounds. Thermal evaporation should not automatically be considered a COD-removal process because volatile organic compounds may transfer into the vapour phase.
2. TDS Concentration: Understand Salt Behaviour During Evaporation
Total Dissolved Solids (TDS) represent the dissolved inorganic and organic constituents present in wastewater. As evaporation removes water, these constituents become increasingly concentrated.
At higher concentrations, certain dissolved salts may approach their solubility limits and begin precipitating, creating scaling and fouling risks.
Key considerations include:
Major dissolved salts and ionic composition
Calcium, magnesium, sulphates, chlorides and silica
Salt solubility at operating temperatures
Boiling point elevation
Potential for precipitation and crystal formation
Corrosion risks associated with concentrated brine
High TDS can increase the boiling point of the solution, affecting the available temperature difference and evaporation capacity. Understanding the complete salt composition is therefore essential when selecting an evaporator configuration.
3. Viscosity: Its Effect on Circulation and Heat Transfer
As organic compounds and dissolved solids become concentrated, wastewater viscosity may increase. Higher viscosity can influence liquid circulation, pumping requirements and heat transfer across evaporator surfaces.
In severe cases, viscous liquids may create poor distribution, uneven heating and difficult solids handling.
Design considerations include:
Feed viscosity at operating temperature
Changes in viscosity during concentration
Circulation velocity and pump selection
Heat-transfer coefficient
Pressure drop across heat-transfer equipment
Maximum practical concentration
Forced-circulation evaporators may be considered for concentrated or difficult-to-handle streams where adequate circulation can be maintained. However, the final selection depends on slurry characteristics, solids loading and operating conditions.
4. Foaming and Entrainment: Protect Vapour Quality
High-COD wastewater may contain surfactants, proteins, oils and other surface-active compounds that promote foaming during evaporation.
Excessive foam can cause liquid droplets to enter the vapour line, a phenomenon known as entrainment. This can contaminate condensate, reduce vapour quality and affect downstream heat-recovery equipment.
Important design considerations include:
Organic composition and surface-active compounds
Foaming tendency at operating temperature
Vapour velocity and vapour-space design
Demister or vapour-separation arrangements
Foam detection and process control
Compatibility and suitability of antifoaming agents
Foaming behaviour should be evaluated using representative wastewater samples. Vapour separators, demisters and suitable operating controls can help minimise entrainment, while chemical antifoam treatment may be considered where appropriate.
5. Scaling and Fouling: Manage Combined Organic and Inorganic Deposits
High-COD, high-TDS wastewater can create multiple fouling mechanisms within the same evaporator.
Inorganic salts may precipitate on heat-transfer surfaces, while organic compounds can form sticky deposits or contribute to surface fouling. Suspended solids may further increase the likelihood of deposition.
Common challenges include:
Calcium carbonate and calcium sulphate precipitation
Silica-related deposits
Organic fouling from oils and process residues
Suspended solids accumulation
Localised concentration and temperature variations
Reduced heat-transfer efficiency
Scaling and fouling control should consider feed pretreatment, circulation, temperature profile, concentration limits and cleaning strategy.
Where necessary, chemical analysis, solubility assessment and laboratory evaporation trials can help identify the dominant deposit-forming compounds before finalising the equipment design.
6. Evaporator Selection: Match the Configuration to the Effluent
Not every evaporator is suitable for every high-COD, high-TDS application. Selection should account for viscosity, foaming, suspended solids, scaling tendency, heat sensitivity and required concentration.
Common configurations include:
Forced Circulation Evaporator (FC): Often considered for concentrated, scaling-prone and solids-bearing streams where controlled circulation is important.
Falling Film Evaporator (FFE): Suitable for compatible low-viscosity liquids requiring efficient heat transfer and relatively short residence times. Feed distribution and surface wetting are important.
Rising Film Evaporator: Can be considered for suitable low-viscosity liquids where vapour generation supports upward film movement through heating tubes.
Multiple Effect Evaporator (MEE): Uses vapour from one effect to heat subsequent effects, helping reduce fresh steam demand.
Mechanical Vapour Recompression (MVR/MVRE): Recompresses suitable secondary vapour for reuse as a heating medium, reducing fresh steam requirements while increasing electrical demand.
The final configuration may involve a combination of technologies, depending on feed characteristics and utility availability.
7. Pretreatment: Improve Feed Conditions Before Thermal Concentration
Pretreatment plays an important role in improving the reliability of downstream evaporation.
Depending on wastewater composition, treatment may include:
Equalisation to manage variations in feed characteristics
Oil and grease separation
Coagulation and flocculation for suitable suspended or colloidal contaminants
Chemical precipitation for selected dissolved constituents
Biological treatment for biodegradable organic matter
UF or other filtration to reduce suspended solids
RO where feed quality and recovery requirements permit
For high-COD streams, a suitable organic-load reduction stage may be beneficial before thermal treatment. For high-TDS streams, dissolved-salt management must also be considered.
Pretreatment selection should be based on wastewater analysis rather than applying the same treatment sequence to every industrial application.
8. Integrating Evaporation with ZLD and Downstream Treatment
For wastewater streams that cannot achieve the required recovery through conventional treatment or membrane processes alone, thermal evaporation can provide an additional concentration stage.
A typical treatment arrangement may include:
Industrial Effluent → Equalisation → Organic and Suspended-Solids Treatment → UF/RO, Where Suitable → RO Reject → Thermal Evaporation → Crystallization, Where Required → Solid-Liquid Separation
The recovered condensate must be assessed for COD, volatile compounds and other contaminants before reuse. Depending on its quality, additional polishing may be necessary.
The concentrated brine may proceed to crystallization, where dissolved salts are converted into solids under controlled conditions. Mother-liquor management and final residue handling must also be incorporated into the overall design.
Key integration factors include:
Organic and inorganic contaminant balance
Evaporator feed quality and concentration
Vapour separation and condensate quality
Energy consumption and heat recovery
Scaling, foaming and corrosion control
Crystallization and solids-separation requirements
Final water reuse and residue-management objectives
An integrated design helps address the interaction between organic loading and dissolved salts while maintaining stable operation across the treatment system.
Engineering High-COD, High-TDS Effluent Treatment with Centpro Engineering
Centpro Engineering approaches complex industrial effluent treatment through process-specific evaluation of COD, TDS, viscosity, foaming tendency, scaling potential and thermal behaviour.
The objective is to identify the appropriate combination of pretreatment, evaporation, vapour separation, crystallization and downstream recovery equipment based on actual wastewater characteristics.
Planning a treatment system for high-COD, high-TDS industrial effluent? Share your wastewater flow rate, COD, TDS, pH, major dissolved salts, suspended solids, viscosity, existing ETP configuration and required water recovery. These details help establish a suitable process configuration for technical evaluation.