
Industrial Crystallizers for Product Recovery and Salt Management
Precision Crystal Formation for High-Purity Recovery and Efficient Resource Utilization
Crystallization is one of the most important separation and recovery operations in modern process industries. From recovering valuable chemicals to managing concentrated salts in Zero Liquid Discharge (ZLD) plants, crystallizer performance directly influences product purity, crystal size, recovery rate, energy consumption, and downstream handling.
As industrial processes become more concentrated and resource-efficient, conventional wastewater treatment alone is often insufficient. High-TDS streams, concentrated mother liquors, and saturated solutions require carefully engineered crystallization systems to convert dissolved solids into recoverable crystals or manageable solid residues.
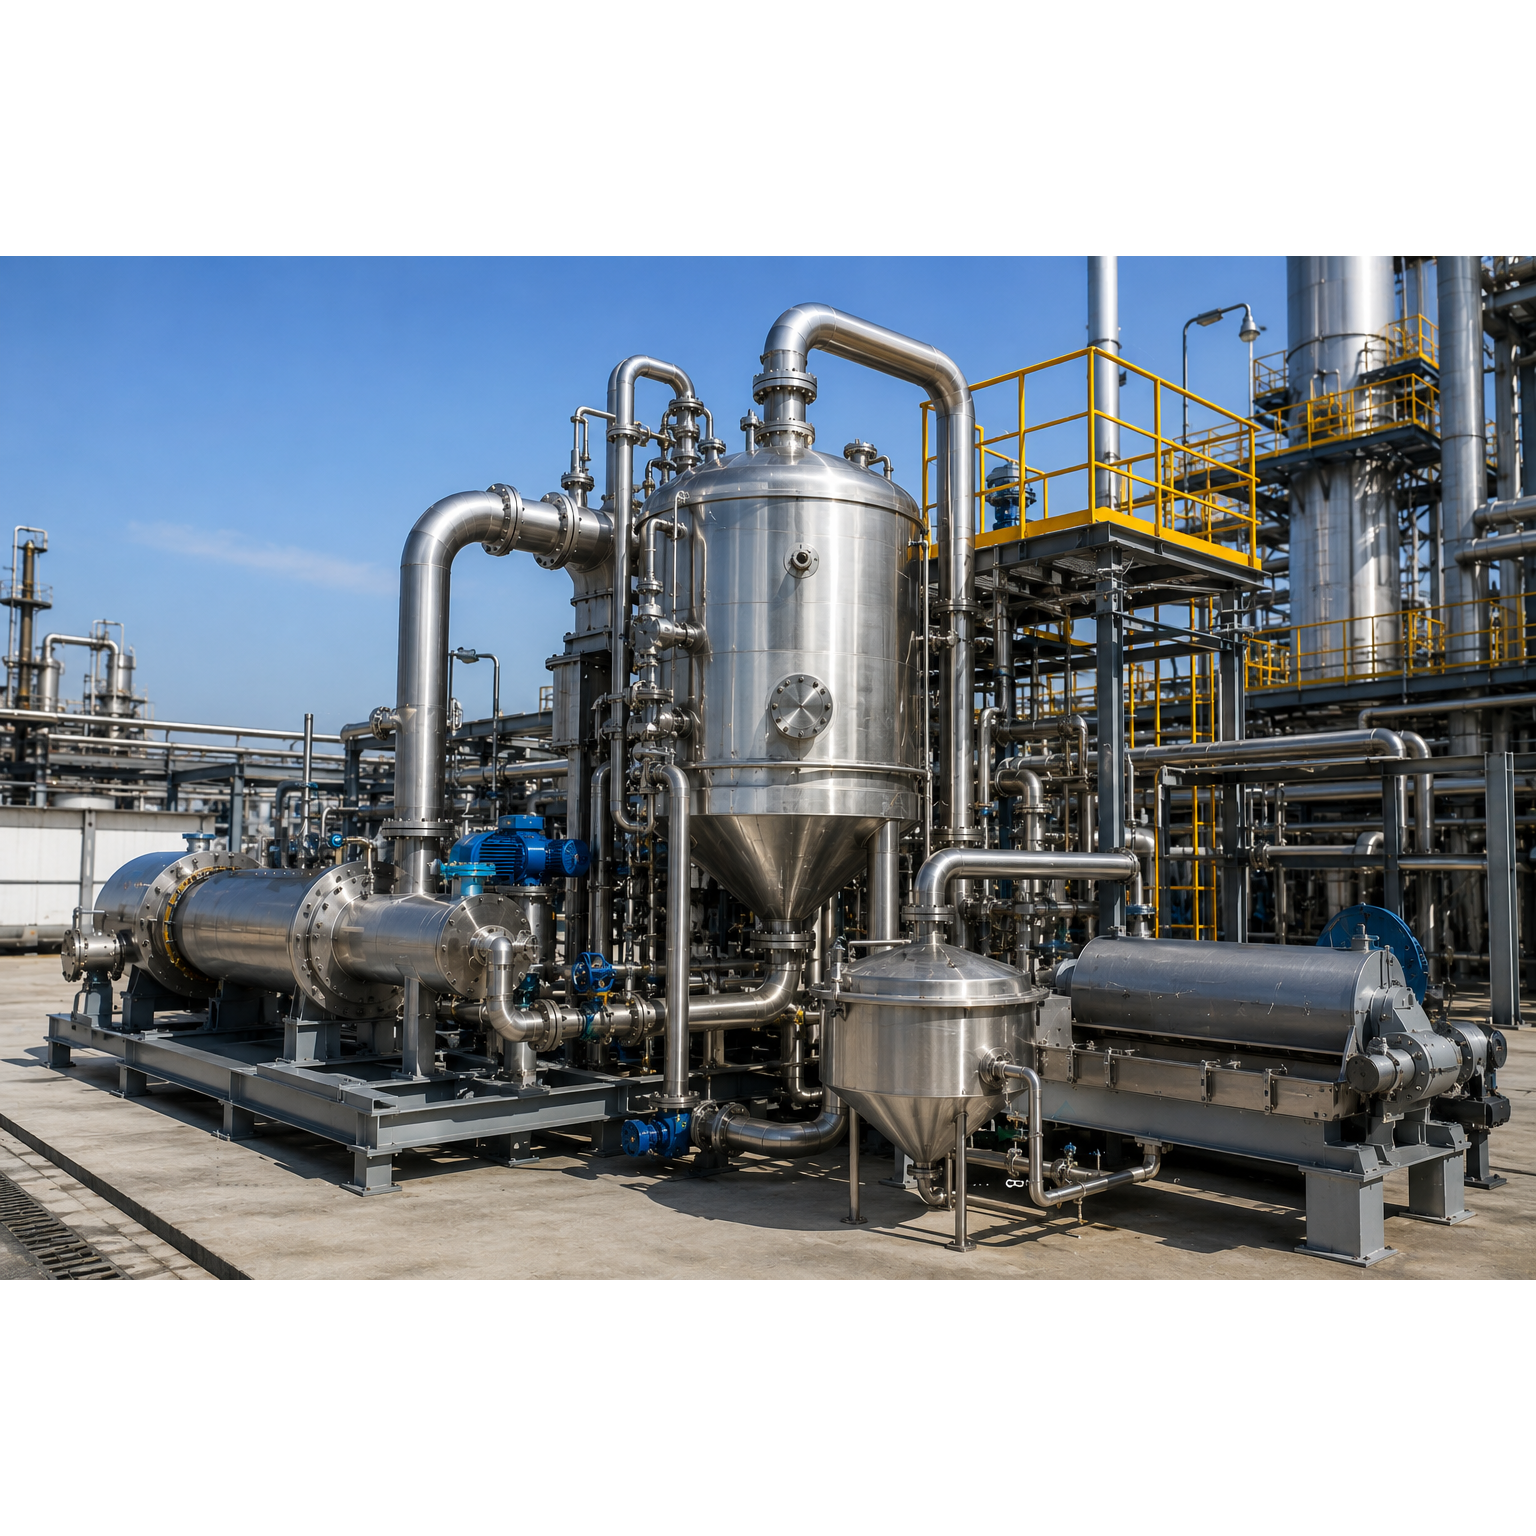
CentPro Engineering Pvt. Ltd. designs and manufactures industrial crystallization systems for chemical, pharmaceutical, fertilizer, specialty chemical, and ZLD applications. Our engineering approach considers feed chemistry, solubility characteristics, concentration levels, scaling tendency, crystal growth behavior, and required recovery to develop a suitable crystallization process.
Understanding Industrial Crystallization
Crystallization involves converting dissolved substances into solid crystals by creating controlled supersaturation within a process stream. The quality of the final crystals depends on how effectively temperature, pressure, concentration, residence time, circulation, and evaporation are controlled.
An improperly designed crystallizer can result in excessive scaling, poor crystal growth, inconsistent particle size, high energy consumption, and difficult downstream separation.
CentPro focuses on controlling these critical process parameters to achieve stable crystallization and reliable solid-liquid separation.
Our Industrial Crystallizer Solutions
Depending on the process chemistry and required operating conditions, CentPro can engineer different crystallization configurations, including:
Forced Circulation Crystallizers
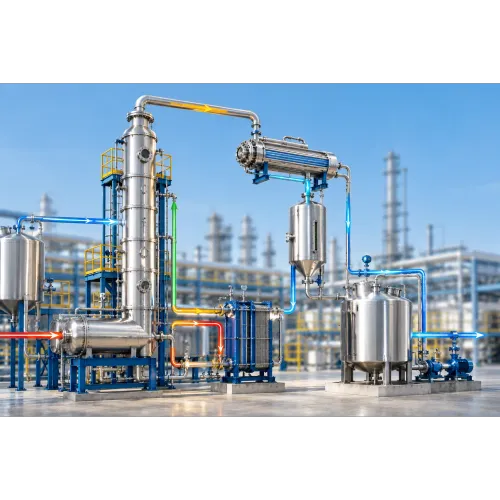
Designed for high-solids and difficult-to-crystallize streams, forced circulation crystallizers maintain high circulation velocities through the heat exchanger to reduce localized supersaturation and minimize uncontrolled scaling.
DTB Crystallizers
Draft Tube Baffle (DTB) crystallizers provide controlled crystal growth and circulation, making them suitable for applications where crystal size distribution and product quality are important.
Vacuum Crystallizers
Vacuum crystallization reduces the boiling temperature by operating under reduced pressure. This makes the technology suitable for heat-sensitive products and applications where lower-temperature evaporation is desirable.
Evaporative Crystallizers
These systems combine evaporation and crystallization to concentrate solutions beyond their saturation point and recover dissolved solids as crystals.
Engineering the Right Crystallizer
There is no universal crystallizer design for every industrial process. The appropriate configuration depends on the physical and chemical characteristics of the feed.
CentPro evaluates parameters such as:
Feed concentration and TDS
Solubility curve
Crystal nucleation behavior
Crystal growth rate
Supersaturation characteristics
Viscosity
Scaling tendency
Heat transfer requirements
Required crystal size
Product purity
Solid-liquid separation requirements
Operating temperature and pressure
Desired recovery rate
This process-specific approach helps achieve predictable crystallization performance and minimize operational problems.
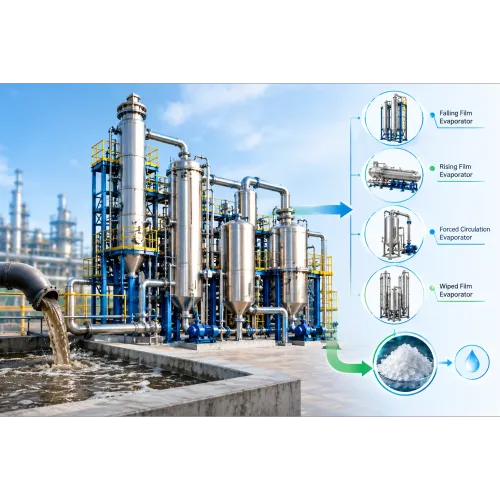
Crystallization in Zero Liquid Discharge Plants
Crystallizers are often the final thermal stage of a ZLD system. After RO and evaporation, the remaining concentrate can contain extremely high levels of dissolved salts.
A typical ZLD process may follow the sequence:
Effluent → Pretreatment → UF → RO → MEE/MVR → Crystallization → Solid-Liquid Separation → Salt Recovery
The crystallizer further concentrates the brine until dissolved salts reach their crystallization point. The resulting crystals can then be separated, dewatered, and managed as solid material.
By integrating crystallization into a ZLD system, industries can significantly reduce liquid waste discharge and maximize water recovery.
Applications Across Process Industries
CentPro crystallization systems can be engineered for a broad range of applications.
Zero Liquid Discharge & Salt Recovery
Recovery and management of salts from concentrated industrial wastewater and RO reject streams.
Chemical Crystallization
Recovery and purification of inorganic and organic chemicals from concentrated process solutions.
Pharmaceutical & API Manufacturing
Controlled crystallization for product purification, isolation, and recovery of pharmaceutical compounds.
Fertilizer Industry
Crystallization and recovery of salts and valuable compounds from fertilizer process streams.
Specialty Chemicals
Recovery of high-value chemical products where controlled crystal size and purity are critical.
Food and Other Process Industries
Concentration and controlled crystallization of selected process streams where product recovery and purity are important.
Key Features
Customized crystallizer design based on process chemistry
Forced circulation configurations for high-solids applications
DTB crystallization for controlled crystal growth
Vacuum operation for lower-temperature crystallization
High circulation rates to minimize localized scaling
Optimized heat transfer systems
Corrosion-resistant material options
Automated temperature, pressure, level, and concentration control
Integration with MEE and MVR evaporation systems
Integration with centrifuges, filters, and dewatering systems
Designed for continuous industrial operation
Suitable for high-TDS and difficult process streams
Improving Recovery While Managing Waste
Modern process industries are increasingly moving toward a circular approach in which waste streams are treated as potential sources of recoverable materials.
A well-engineered crystallization system can help industries:
Recover valuable chemical products
Reduce liquid waste volume
Improve overall water recovery
Recover salts from concentrated brine
Reduce disposal requirements
Improve product purity
Optimize downstream separation
Support Zero Liquid Discharge objectives
CentPro's Integrated Crystallization Expertise
CentPro Engineering combines process engineering, thermal system design, equipment manufacturing, and automation capabilities to develop integrated crystallization solutions.
Our crystallizers can be integrated with MEE, MVR, RO, ZLD, condensate recovery, and downstream solid-liquid separation systems, allowing the complete process to operate as a coordinated treatment and recovery system.
Rather than selecting crystallization equipment based only on capacity, CentPro evaluates the complete process—from feed characteristics and concentration through crystal formation, separation, dewatering, and final product or salt handling.
Designed for Reliable Industrial Operation
Crystallization systems often operate under demanding conditions involving high temperatures, concentrated salts, corrosive chemicals, and high solids loading. Equipment design therefore requires careful consideration of metallurgy, heat transfer surfaces, circulation velocity, scaling control, mechanical integrity, and maintenance accessibility.
CentPro can engineer equipment using suitable materials and configurations based on the chemical characteristics and operating conditions of the process.
Why Choose CentPro?
CentPro Engineering provides customized crystallization solutions backed by process engineering and equipment manufacturing expertise. Our objective is to develop systems that deliver reliable crystal formation, efficient recovery, controlled energy consumption, and long-term operational performance.
From individual industrial crystallizers to complete ZLD and chemical recovery plants, CentPro supports clients through process engineering, equipment design, manufacturing, integration, installation, commissioning, and technical support.