
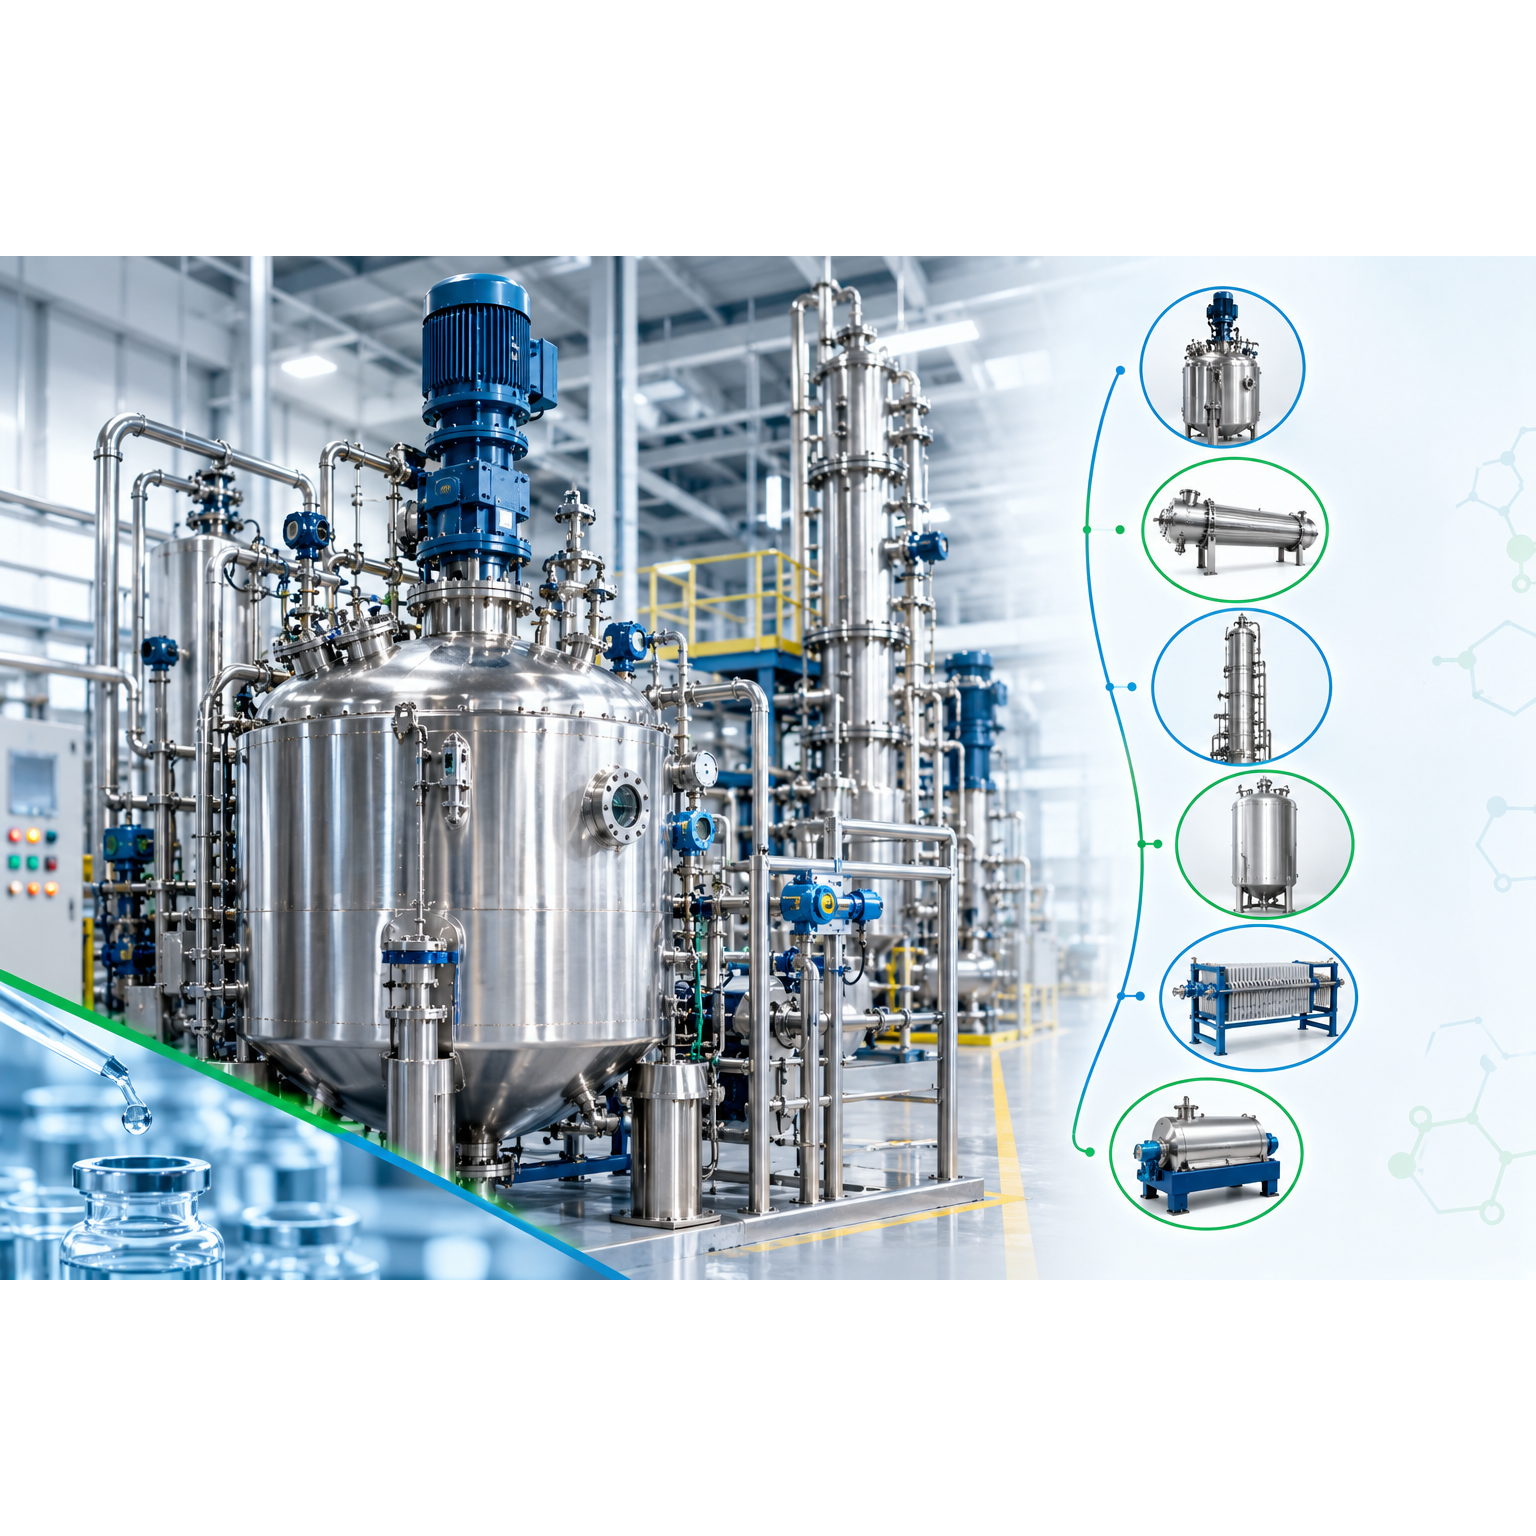
In chemical and pharmaceutical manufacturing, selecting process equipment involves more than defining capacity, pressure and temperature. The equipment must perform reliably under the actual process conditions, maintain product quality and support safe, efficient and consistent operation.
The right equipment begins with understanding the process requirement.
At Centpro Engineering, process equipment selection is approached by evaluating the material being handled, the required process outcome and the operating challenges that influence performance.
1. Reactors: Designed Around Reaction Requirements
Reactor selection depends on reaction chemistry, batch volume, operating pressure, temperature control, agitation and heat-transfer requirements. Viscosity, solids content and reaction time also influence vessel geometry and impeller selection.
For chemical and pharmaceutical applications, material compatibility and effective heating or cooling are essential to achieving consistent process performance.
2. Heat Exchangers: Designed Around Heat Duty
Heat exchangers must match the required heat duty, inlet and outlet temperatures, operating pressure and process-fluid characteristics. Fouling tendency, corrosion resistance and allowable pressure drop influence the design.
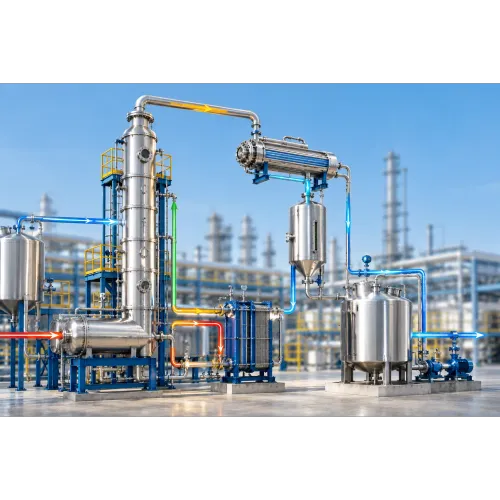
For difficult applications, proper heat integration can also reduce utility consumption by recovering energy from suitable process streams.
3. Evaporators: Selected for Concentration and Energy Efficiency
Evaporator selection depends on feed flow, TDS, viscosity, boiling-point elevation, scaling tendency and heat sensitivity.
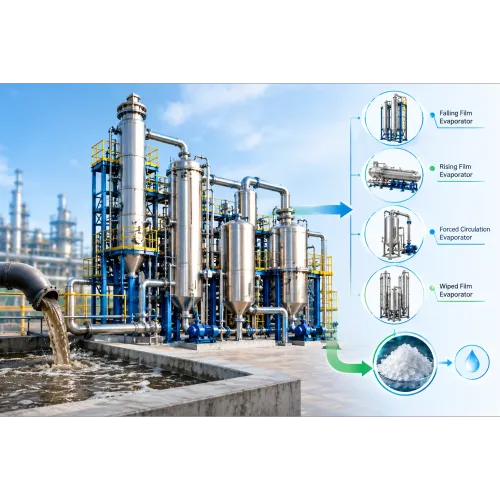
Falling-film evaporators may suit relatively clean, low-viscosity feeds, while forced-circulation systems are often considered for concentrated, scaling-prone liquids. MEE and MVR/MVRE configurations are evaluated according to process conditions, steam availability, electrical power consumption and operating economics.
4. Filters: Matched to Separation Requirements
Filtration depends on particle size, solids loading, liquid viscosity, cake characteristics and the required filtrate quality.
Cartridge filters, Nutsche filters and other industrial filtration systems serve different separation requirements. The selection must consider filtration area, pressure drop, solids handling, cleaning requirements and material compatibility.
5. Crystallizers: Controlled Solid Formation
Crystallizer design depends on solubility, supersaturation, temperature, circulation, residence time and the desired crystal size and quality.
In chemical processing and ZLD applications, these factors influence salt recovery, downstream solid-liquid separation and the performance of integrated evaporation systems.
6. Separation Equipment: Designed for Product Purity
Distillation columns, solvent recovery systems, condensers and related separation equipment are selected according to feed composition, relative volatility, required purity, recovery targets and thermal sensitivity.
Reflux ratio, operating pressure, stage efficiency and heat integration influence both separation performance and operating cost.
An Integrated Process Approach
These equipment systems rarely operate independently. A reactor may feed a filtration system; the filtrate may undergo evaporation; concentrated material may enter a crystallizer; and the resulting solids may require further separation and drying.
Equipment selection must therefore consider the complete process—not just the individual machine.
Centpro Engineering supports process design, detailed engineering, equipment manufacturing, instrumentation and control, installation and commissioning for chemical, pharmaceutical and other process industries.
Our approach considers material of construction, operating conditions, heat and mass transfer, energy consumption, maintainability and downstream process requirements before finalizing the equipment configuration.
Planning a Challenging Process Application?
Share your process flow, feed composition, required production capacity, operating temperature and pressure, material compatibility requirements and desired product quality.
Centpro Engineering can evaluate the process requirements and develop a suitable equipment or integrated process solution around your application.