
Engineering Reactors for Demanding Chemical Processes
A reactor is more than a fabricated vessel—it is the core of the chemical process where controlled reactions determine product quality, yield, safety, and production efficiency. Selecting the right reactor configuration requires a detailed understanding of reaction chemistry, heat transfer, mixing, pressure, temperature, residence time, material compatibility, and operating conditions.
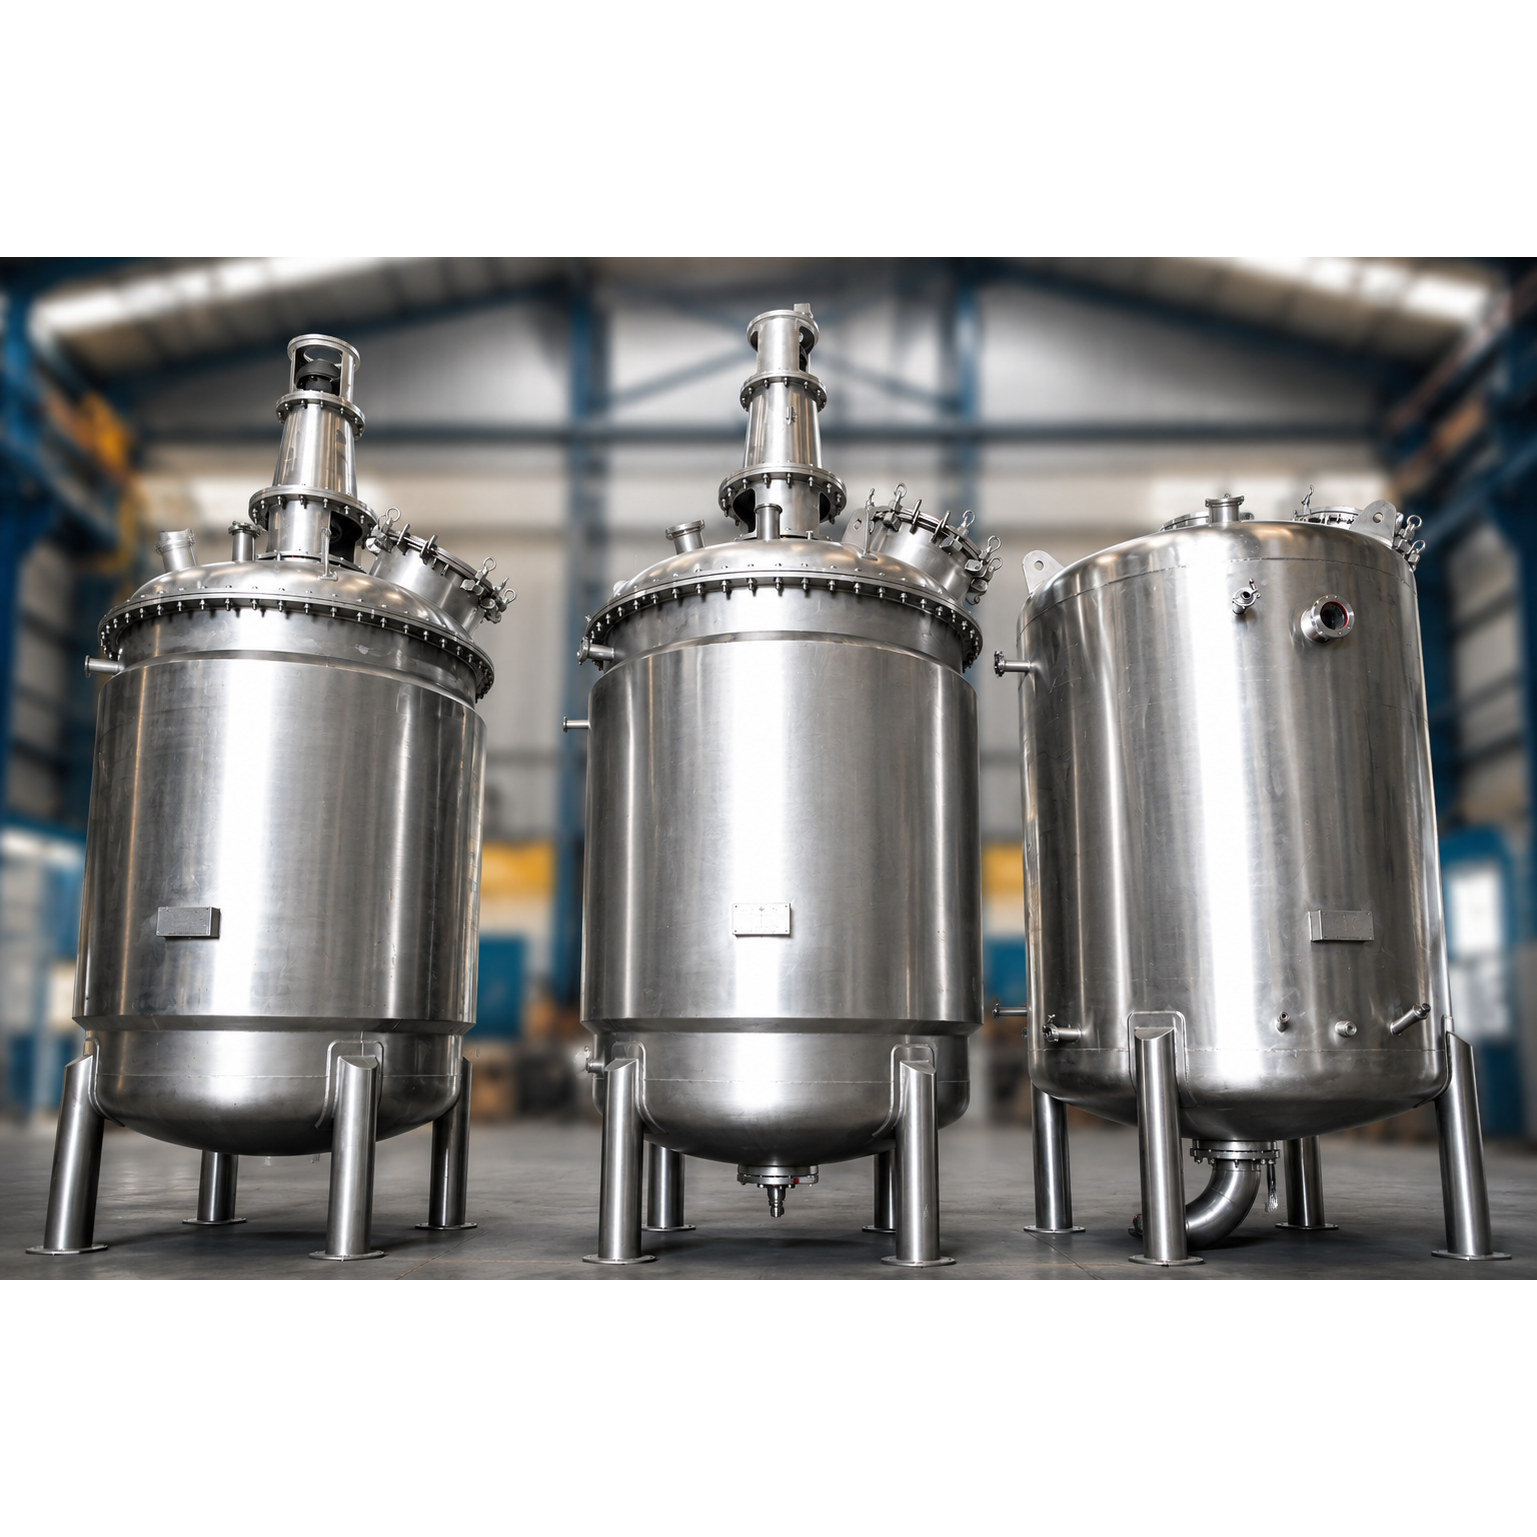
Centpro Engineering Pvt. Ltd. designs and manufactures industrial chemical reactors and process reaction vessels for chemical, pharmaceutical, specialty chemical, agrochemical, food, and allied process industries. Our approach combines process engineering with mechanical design and precision fabrication to develop reactors suited to the actual requirements of each application.
Reactor Design Starts with the Process
No two chemical reactions behave exactly the same. Exothermic reactions may require rapid heat removal, while endothermic processes may demand controlled heating. Highly viscous materials require effective agitation, while sensitive reactions may need precise temperature and residence-time control.
Before finalizing reactor design, critical parameters such as the following are evaluated:
- Reaction chemistry
- Batch size and production capacity
- Operating temperature
- Design and operating pressure
- Vacuum requirements
- Heat generation or absorption
- Mixing requirements
- Viscosity and density
- Residence time
- Corrosion characteristics
- Material compatibility
- Heating and cooling requirements
- Cleaning and maintenance requirements
This process-driven approach ensures that the reactor is engineered around the reaction, rather than simply selecting a standard vessel.
Reactor Configurations
Centpro can design customized reactor systems based on process requirements and operating conditions.
Jacketed Reactors
Jacketed reactors provide controlled heating and cooling through a surrounding jacket. They are widely used for batch chemical reactions where accurate temperature control is critical.
Limpet Coil Reactors
Limpet coil arrangements provide an effective heat-transfer surface around the reactor shell and can be selected for applications requiring heating or cooling during the reaction cycle.
Vacuum Reactors
Vacuum-capable reactors are used for processes involving vacuum evaporation, solvent removal, drying, degassing, or reactions that benefit from reduced operating pressure.
Pressure Reactors
For reactions requiring elevated pressure, reactors are designed considering the required design pressure, temperature, mechanical integrity, nozzle configuration, and applicable design standards.
Materials of Construction
Material selection is one of the most important aspects of reactor engineering. The wrong material can lead to corrosion, contamination, premature failure, or increased maintenance costs.
Depending on the process chemistry, CentPro can work with materials such as:
- SS304
- SS316
- SS316L
- Duplex Stainless Steel
- Super Duplex Stainless Steel
- Hastelloy and other nickel alloys
- Titanium
- Other specialized materials based on process requirements
Material selection is determined by factors such as chemical concentration, chloride content, temperature, pH, pressure, corrosion potential, and product compatibility.
Agitation & Mixing: The Heart of Reactor Performance
A reactor can have excellent heat-transfer characteristics and still deliver poor results if the mixing system is incorrectly designed.
Centpro considers factors such as viscosity, density, solids content, reaction kinetics, gas-liquid interaction, and required mixing intensity when developing the agitation system.
Possible configurations include:
- Anchor agitators
- Paddle agitators
- Turbine agitators
- Propeller agitators
- High-shear mixing systems
- Customized agitator designs
The agitator, motor, gearbox, shaft, impeller, and mechanical seal are selected as an integrated system.
Heating and Cooling Systems
Maintaining the correct reaction temperature is critical to achieving consistent product quality and reaction efficiency.
Centpro reactors can be integrated with heating and cooling systems using:
- Steam
- Hot water
- Thermal fluid
- Chilled water
- Cooling water
- Other process-specific heating/cooling media
The reactor's heat-transfer system is designed according to the required temperature range, heat duty, batch cycle, reaction kinetics, and available utilities.
Batch and Continuous Reactor Applications
Centpro engineers reactor systems for both batch and continuous manufacturing processes.
Batch Processing
Batch reactors provide flexibility for multiproduct chemical plants and are commonly used in:
- Specialty chemicals
- Pharmaceuticals
- API manufacturing
- Resins
- Adhesives
- Dyes and pigments
- Agrochemicals
Continuous Processing
Continuous reactor systems can provide consistent production, controlled residence time, and higher process throughput for suitable chemical reactions.
Scale-Up from Laboratory to Production
Scaling a reaction from laboratory or pilot level to industrial production is not simply a matter of increasing vessel volume.
Changes in vessel geometry can influence:
- Mixing performance
- Heat-transfer rate
- Reaction temperature
- Mass transfer
- Residence time
- Power consumption
- Reaction kinetics
- Product consistency
Centpro's process engineering approach considers these factors while developing production-scale reactor systems, helping bridge the gap between laboratory development and industrial manufacturing.
Customized Reactor Equipment
Depending on the process, a reactor package may include more than the reactor vessel itself.
Centpro can integrate:
Reactor → Agitator → Heating/Cooling System → Condenser → Receiver → Vacuum System → Instrumentation → Automation
Additional equipment such as pumps, filters, heat exchangers, dosing systems, condensers, and process skids can also be incorporated where required.
Applications
Our industrial reactor systems can be engineered for:
- Chemical Manufacturing
- Specialty Chemicals
- Pharmaceutical Manufacturing
- API Production
- Agrochemicals
- Dyes & Pigments
- Paints & Resins
- Adhesives
- Petrochemicals
- Food Processing
- Biotechnology
- Pilot and Scale-Up Plants
From Reactor Manufacturing to Complete Process Integration
Centpro's capability extends beyond reactor fabrication. Our process engineering and project execution expertise allows reactors to be integrated into complete manufacturing systems involving piping, heat exchangers, distillation systems, solvent recovery, filtration, utilities, instrumentation, automation, and plant commissioning.
This integrated approach helps ensure that the reactor performs as part of the complete process rather than as an isolated piece of equipment.
Why Choose Centpro for Industrial Reactors?
Centpro Engineering combines process understanding, mechanical design, material selection, fabrication, equipment integration, and project execution to manufacture customized reactor systems for demanding industrial applications.
Whether the requirement is a compact pilot reactor, a pharmaceutical-grade process vessel, or a large-scale chemical reaction system, our focus remains the same: safe operation, reliable mixing, efficient heat transfer, material compatibility, maintainability, and consistent process performance.